
Retail Solutions
Fresh & Frozen Food Manufacturing Capabilities
Today's consumers demand convenience, quality, freshness, and value. Food brands and operators need a manufacturing partner capable of delivering innovation, scalability, food safety, and operational excellence. We help leading brands, retailers, foodservice operators, and emerging food companies develop, commercialize, manufacture, and scale fresh prepared foods, refrigerated meal solutions, frozen prepared foods, grab-and-go programs, meal kits, and private label products. Whether you are seeking a co-manufacturer, contract manufacturer, private label supplier, co-packer, or innovation partner, we provide the culinary expertise, manufacturing capabilities, national footprint, and food safety systems required to bring products to market successfully.
End-to-End Product Development & Rapid Commercialization
Successful food programs begin with consumer insights, culinary creativity, and operational expertise.
Our culinary innovation and product development teams work alongside customers to transform ideas into scalable, profitable products. From custom formulation and concept development through commercialization and manufacturing scale-up, we help customers accelerate speed-to-market while maintaining quality, consistency, and cost objectives.
Whether launching a new product line, seasonal LTO, private label program, or national menu platform, we help customers move from concept to commercialization with confidence.
Capabilities
Culinary innovation and menu development
Product ideation and concept creation
Custom formulation
Consumer trend analysis
Prototype development
Shelf-life optimization
Cost engineering
Packaging optimization
Manufacturing scale-up
Rapid commercialization
Turnkey product development support
Fresh Prepared Food Manufacturing
We specialize in fresh prepared foods designed for today's convenience-driven consumer.
Our refrigerated manufacturing capabilities support short shelf-life, fresh prepared, clean-label, and retail-ready programs for both food service and retail channels.
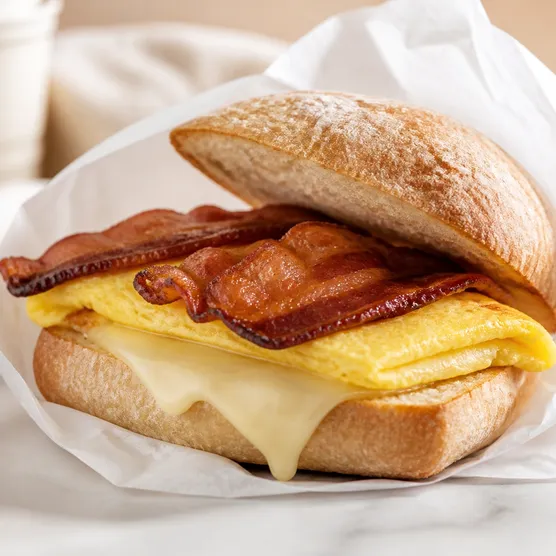
Our manufacturing platforms support:
Sandwiches & Handhelds
Fresh sandwiches
Breakfast Sandwiches
Specialty sandwiches
Paninis
Wraps
Handheld meal solutions
Refrigerated Grab-and-Go Programs
Grab-and-go meals
Retail-ready meal solutions
Fresh prepared snacks
Convenience store food programs
Fresh breakfast offerings
Salads & Healthy Prepared Foods
Prepared salads
Protein salads
Premium salad bowls
Fresh meal solutions
Better-for-you offerings
Snacks & Protein Solutions
Protein boxes
Snack packs
Fresh fruit programs
Yogurt parfaits
Portion-controlled snacks
Meal Kits & Fresh Prepared Meals
Fresh meal kits
Portion-controlled meal components
Frozen Food Manufacturing
As consumer demand for convenience, labor savings, and extended shelf life continues to grow, frozen prepared foods have become one of the fastest-growing categories across retail and foodservice.
Our frozen manufacturing platform helps customers extend shelf life, reduce waste, improve distribution efficiency, and support national product launches.
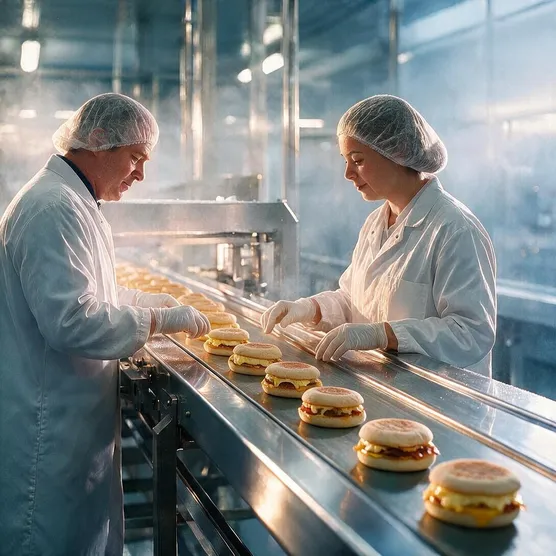
Our frozen capabilities include:
Frozen Handhelds
Frozen breakfast sandwiches
Frozen breakfast burritos
Frozen wraps
Frozen handheld meals
Frozen convenience foods
Retail & Club Store Programs
Warehouse club programs
Pallet-ready products
Retail-ready frozen foods
Foodservice Solutions
Frozen foodservice packs
Bulk-pack prepared foods
Institutional meal solutions
Labor-saving products
Heat-and-serve programs
An Extension of Your Team
Whether you need additional capacity, specialized capabilities, or a complete turnkey manufacturing solution, we provide flexible co-manufacturing and private label support tailored to your business. Our services include: • Co-manufacturing • Contract manufacturing • Private label manufacturing • Store-brand programs • Co-packing services • Product commercialization • Procurement support • Packaging solutions • Regulatory compliance • Quality assurance management We support emerging brands, regional operators, national retailers, and large foodservice organizations with customized manufacturing programs built around their specifications, brand standards, and growth objectives. Private Label Expertise We help customers develop: • Retail private label products • Store-brand programs • Exclusive retail offerings • Club-store private label products • Foodservice-exclusive programs • Regional and national branded products Every program is designed to meet the unique needs of the customer, channel, and consumer.
Fresh, frozen, and extended shelf life under one roof — one partner, every format
National Manufacturing Network
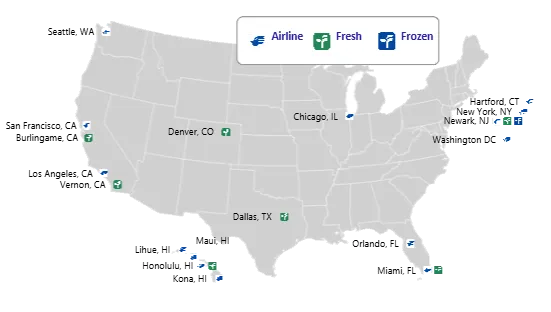
Our manufacturing network is designed to support both regional and national food programs.
This network enables customers to grow efficiently while reducing transportation complexity and improving service levels.
Benefits include
Multi-site manufacturing
National footprint
Regional production capabilities
National distribution support
High-volume manufacturing
Food Safety, Quality & Regulatory Compliance
Protecting consumers and customer brands is our highest priority. Our food safety and quality systems are built around industry-leading standards, rigorous verification, and continuous improvement Food Safety & Compliance Programs • SQF-certified facilities • HACCP-based food safety systems • USDA-inspected operations • FDA-compliant programs • FSMA compliance • Full traceability systems • Allergen control programs • Environmental monitoring programs • Supplier qualification programs • Product testing protocols • Recall readiness procedures Proven Performance • Consistently strong audit performance • Robust regulatory compliance systems • Strong customer quality metrics • Comprehensive food safety culture • Continuous quality improvement initiatives Customers trust us to protect their brands, consumers, and reputations.
Supply Chain & Procurement Excellence
Our procurement and supply chain teams support customers through: • Strategic sourcing • Supplier qualification • Ingredient procurement • Inventory management • Demand planning • Forecasting support • Distribution network coordination • Sustainability-focused sourcing Our extensive supplier network helps ensure reliable ingredient availability, quality consistency, and operational flexibility.
120M+ meals produced annually
Why Leading Brands Choose Us
Innovation Culinary-led product development, custom formulation, menu innovation, and commercialization expertise. Manufacturing Excellence Fresh and frozen food manufacturing capabilities designed for consistency, quality, and scale. Food Safety Leadership SQF-certified facilities, HACCP programs, USDA compliance, traceability systems, and rigorous quality controls.
National Scale Multi-site manufacturing, regional production capabilities, and national distribution support. Flexible Partnership Model Co-manufacturing, contract manufacturing, co-packing, and private label solutions customized to your needs. Customer-Centric Approach Responsive service, rapid customization, operational agility, and long-term partnership focus.
Let's Build What's Next
Whether you're seeking a fresh prepared foods supplier, frozen prepared foods manufacturer, private label partner, co-manufacturer, meal kit assembly provider, or national food manufacturing partner, we're ready to help.
Ready to Launch, Scale or Optimize Your Food Program?
Email Us - Sales Inquiries
Sales Inquiries
(206) 624-9576
Customer Service Hours
9:00 AM - 4:00 PM PT
Address